Hey there, fellow optical component pros and injection moulding enthusiasts! If you’ve ever dabbled in making eyeglass frames, you know that even the tiniest tweak in your moulding process can turn a crisp, high-precision frame into a warped, unusable mess. As someone who’s been an optical frame injection moulding machine supplier for over a decade—chatting with lab managers, production leads, and quality control folks every single day—I can’t tell you how many times I’ve heard, “Back pressure… what’s the big deal? I just crank it to ‘good enough’ and call it a day.” Spoiler alert: that “small” setting could be the reason your frames are cracking around the lens mounts, have uneven thickness, or are getting rejected at final inspection left and right. Today, let’s break down exactly what back pressure does on an optical frame injection moulding machine, why it’s non-negotiable for this specific industry, and how to nail that setting without overcomplicating it. Optical Frame Injection Moulding Machine
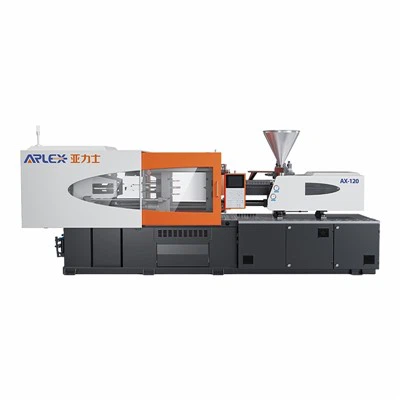
First, let’s keep this real—no jargon that makes your eyes glaze over. When you run an injection moulding machine for optical frames, you’re not making plastic toys or food containers. These frames need to be super precise: consistent thickness, smooth edges, no bubbles, and enough structural integrity to hold up to daily wear. That’s why the process is way trickier than most people think, and back pressure is one of the unsung heroes behind that precision. Let’s start with the basics of how the machine works, super simplified: when you load plastic resin (usually polycarbonate, optrex, or TR-90, the go-tos for eyewear) into the machine’s barrel, a screw rotates to melt it into a thick, slush-like liquid. Then, the screw pushes that molten plastic into the closed mould. But back pressure is the tiny, controlled force that pushes back on that screw while it’s rotating to melt the plastic. It’s not the same as the high-speed injection force that blasts plastic into the mould—that’s a common mix-up! Think of it like squeezing a tube of toothpaste: you push the tube (that’s the injection force), but if you also apply gentle, consistent pressure on the plunger while you squeeze, you get a smoother, more even stream. That’s back pressure in a nutshell.
Now, why is this so critical for optical frames specifically? Let’s get into the nuts and bolts of what back pressure actually achieves here. First up: it mixes the molten resin properly. Wait, but why does mixing matter so much for eyeglass frames? If the resin isn’t mixed evenly, you’ll have hot spots where some plastic is over-melted and too soft, or cold spots where it’s still a little solid. For frames, that translates to uneven shrinkage after cooling. And if you’ve ever had a frame shrink unevenly, you know what happens: one side is tighter than the other, it warps when you put lenses in, or it cracks within a month of the customer wearing it. Back pressure makes the molten plastic more homogenous by pushing the resin particles together, so they don’t separate as they melt. For example, if you’re using TR-90, a flexible polyamide resin popular for lightweight frames, inconsistent mixing can make some parts too rigid and others too bendy—hard no for a product that’s supposed to be comfortable and durable.
Next, back pressure eliminates air bubbles. When the screw is rotating and melting plastic, air can get trapped in the molten resin, right? Those bubbles are a disaster for optical frames. Not only do they create weak spots that lead to cracking, but they can also leave tiny, visible imperfections on the frame’s surface—something you can’t hide with paint or polishing, especially on clear or semi-transparent frames (super trendy right now). How does back pressure fix this? The controlled force from back pressure compacts the molten plastic, squeezing out any trapped air before it gets injected into the mould. I’ve seen this first-hand with a customer in Milan a couple years back: they were cranking their injection speed way up to meet production quotas, and their frames had a 12% defect rate because of surface bubbles. We tweaked their back pressure from 8 bar to 12 bar (don’t worry, we’ll get to setting numbers later) and their defect rate dropped to under 2% overnight. Game changer, yeah?
Another big one: it stabilizes the melt volume and temperature. Here’s the thing: optical frame moulds are tiny, with super precise cavities for the lens edges, the bridge, and the temple arms. If your melt volume (how much plastic you’re injecting) is off by even 0.1 cc, that’s enough to make a frame that’s too bulky or too thin around the lens mount, which means lenses won’t fit right. Back pressure helps keep the screw’s final position consistent at the end of the injection cycle. Without enough back pressure, the screw might “slip” a little when it’s moving forward, leading to inconsistent shot sizes. Same with temperature: if the molten plastic is all different temperatures when it hits the mould, the cooler parts will solidify faster than the hotter parts, leading to uneven cooling and warping. Back pressure ensures the plastic is sheared evenly as the screw rotates, which keeps the melt temperature uniform throughout the entire batch. For high-volume production runs (like 500 frames a day), that consistency is everything—one bad batch can cost you thousands in wasted resin and lost orders.
Wait, but let’s not pretend back pressure is a “set it and forget it” kind of setting. A lot of operators think “more is better,” but that’s a quick path to disaster. If you crank back pressure too high, what happens? Let’s list the pain points we see with our clients all the time. First, you get too much shear heat. Shear heat is the heat generated when the molten plastic rubs against the barrel wall and the screw. Too much back pressure means the screw is working way harder, generating extra heat that can degrade the resin. For example, polycarbonate resin starts to break down if it’s heated above 300°C, and degraded polycarbonate makes frames that are brittle, yellow over time, or prone to cracking. I had a customer in Tokyo last year who increased back pressure to 20 bar to fix a bubble problem, and ended up with yellow frames that got returned within weeks—turned out the resin was burning from excess shear heat from too much back pressure.
Then, too much back pressure can shorten the life of your machine and moulds. The extra force on the screw and barrel means more wear and tear, so you’re replacing parts way more often than you need to. And for the moulds—those are precision tools that cost a small fortune (we’re talking $5,000 to $15,000 per mould, depending on frame complexity). The extra force from too much back pressure can stress the mould’s cavities, leading to tiny cracks that show up on your frames, or even warped moulds that are useless. Finally, too much back pressure slows down your production cycle. Wait, what? I thought more pressure would make things faster. No—when the screw has to push against extra back pressure, it takes longer to rotate and melt the right amount of plastic. So instead of a 20-second cycle per frame, you’re looking at 25 or even 30 seconds, which cuts into your daily output. That’s a big hit for a business that’s counting on meeting deadlines.
So how do you nail the perfect back pressure setting for optical frames? Let’s keep this practical, with actionable steps I share with every client that buys a machine from us. First, start low. We usually recommend a baseline of 5 to 10 bar for most common optical frame resins (TR-90, polycarbonate, optrex). Don’t jump straight to high numbers—tweak in small increments, like 1 or 2 bar at a time. Second, monitor your melt consistency. After each shot, check the plastic coming out of the nozzle (the tip of the machine where plastic comes out before entering the mould). If it’s smooth and uniform, that’s good. If it has streaks or looks lumpy, you need a little more back pressure. Third, track your defect rates. We use a simple checklist with our clients: note the number of bubble defects, warped frames, brittle frames, or surface imperfections every hour. If you’re seeing bubbles, bump back pressure up by 1 bar. If you’re seeing yellow frames or wear on the mould, bump it down by 1 bar. Fourth, match back pressure to your specific resin and frame design. For flexible, thin temple arms, you might need a little lower back pressure so the resin flows smoothly into those tiny cavities. For thick, heavy frames, a little higher back pressure to ensure the plastic fills every corner of the mould. For clear or colored frames, keep back pressure on the lower side to avoid shear heat that causes yellowing.
Also, don’t forget to pair back pressure with other settings that work for optical frames. It’s not a solo act. For example, injection speed: if you’re using low back pressure, you might need a slightly slower injection speed to avoid air bubbles. If you’re using high back pressure, you can crank up injection speed a little to keep the cycle time short. Mould temperature is another big one—cooler moulds mean faster solidification, so you might need a little more back pressure to make sure the plastic fills the mould before it cools. It’s all a balance, and that’s what we help our clients nail when we do on-site training.
Now, let’s get real about why this matters for your bottom line. When you get back pressure right, you’re looking at lower defect rates, less wasted resin, longer machine and mould life, and more consistent, high-quality frames that customers actually buy and don’t return. I’ve had clients go from 10%+ defect rates to under 2% just by tweaking their back pressure setting. That translates to thousands of dollars saved, and a much better reputation in the eyewear industry. Because let’s be honest: in optical frames, quality is everything. A customer will choose a frame that fits perfectly, looks great, and doesn’t warp over one that’s cheap but full of defects. So getting every setting right, including back pressure, is non-negotiable.
If you’re still scratching your head, or if you’re dealing with those stubborn frame defects that just won’t go away, don’t guess. As an optical frame injection moulding machine supplier, we’ve worked with hundreds of labs and production facilities, and we know the ins and outs of every setting, especially back pressure. We can walk you through a step-by-step setup, adjust your existing machine settings, or even customize machine configurations for the specific frames you make. No jargon, no pushy sales talk—just real solutions that help you make better frames, faster, with fewer headaches.
So if you’re ready to stop fighting stubborn defects, cut down on wasted material, and boost your production consistency, reach out to our team to chat. We’re here to help you get your back pressure (and every other setting) dialed in for exactly what your optical frames need. Let’s make your production run smoother, your frames better, and your business more successful.
Plastic Injection Moulding Machine References
Rosato, D. V., & Rosato, M. G. (2000). Injection Molding Handbook. Springer.
Beaumont, J. P. (2015). Injection Molding: Technologies and Fundamentals. Hanser Publications.
Optical Engineering. (2018). Precision Molding of Eyewear Components. SPIE Digital Library.
Ningbo Yalishi (Arlex) Plastic Machinery Co., Ltd.
Address: No.63, Huangsu East Road, Industrial Zone, Dongqian Lake Tourist Resort, Ningbo, Zhejiang Province
E-mail: leo@arlex.cn
WebSite: https://www.arleximm.com/
