If you’ve ever stood at the edge of a mid-sized steel mill at dawn, watching sparks fly from a blast furnace’s open tap, you’ve witnessed air separation unit (ASU) technology at work—even if you didn’t know it. For 15 years, I’ve been a regional ASU supplier, troubleshooting leaky distillation columns, tuning cryogenic cycles, and walking steel plant managers through the math of why their production line is stalling because of a missing stream of high-purity oxygen. What most people outside metallurgy don’t realize is that ASUs aren’t just “air filters for heavy industry”: they’re the quiet backbone of every process that turns raw ore into the steel, aluminum, and other metals that build our cities. Today, I want to break down how ASU tech has evolved from a niche mid-20th-century invention to a make-or-break factor for metallurgical operations’ efficiency, cost, and carbon footprint—and how partnering with the right ASU supplier can turn that impact into a competitive advantage. Type Of Air Separation Unit
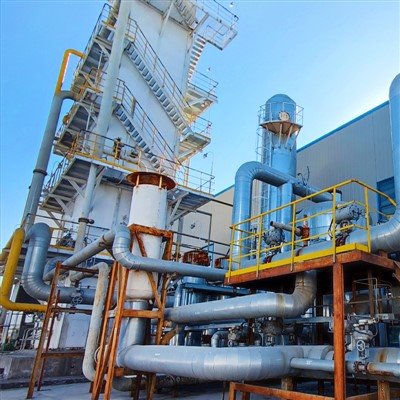
Let’s start with the basics to ground this. Metallurgy, at its core, is about purifying metal oxides (ore) to get usable metal, and that reaction almost always needs oxygen. Early 1900s steel mills pulled oxygen for blast furnaces by burning coke in air, a crude method that only delivered ~28% oxygen at best, wasted 70% of the air as nitrogen, and produced tons of excess CO₂. Then, in the 1950s, cryogenic air separation hit the market: the process of cooling air to -196°C (its liquefaction point), then distilling it into its components—78% nitrogen, 21% oxygen, 1% argon—by exploiting each gas’s unique boiling point. For metallurgy, this was a revolution. Suddenly, mills could pump in 95%+ pure oxygen to blast furnaces, cutting the amount of coke needed per ton of steel by 15% overnight and boosting production by 10% because the furnace burned hotter and faster.
But that first generation of cryogenic ASUs was far from perfect. They were massive—some took up half a football field—required constant round-the-clock maintenance, and guzzled so much energy that 40% of a mill’s total electricity bill went to powering its ASUs. By the early 2000s, as global steel demand surged and climate regulations started to tighten, metallurgists realized they needed ASUs that could do more than just produce oxygen. They needed ASUs that adjusted on the fly, cut waste, and integrated with their entire production line. That’s when I started seeing a shift in my work as a supplier: clients stopped asking for “big enough ASUs” and started asking for ASUs that could “keep up with our furnace’s variable output.”
This brings us to the modern ASU technologies that are reshaping metallurgy right now. First, let’s talk about pressure swing adsorption (PSA) and vacuum pressure swing adsorption (VPSA) ASUs, which are the biggest game-changers for smaller and mid-sized metallurgical operations. Unlike cryogenic ASUs, which are best for plants producing 100+ tons of metal per day, PSA ASUs use carbon molecular sieves (CMS) to separate oxygen from nitrogen at room temperature, using pressure changes instead of cold. When I installed a VPSA ASU for a 200-ton-per-day aluminum smelter in western Ohio in 2019, the client’s annual energy bill for oxygen dropped by 32% compared to their old cryogenic unit—savings that let them hire three extra shift supervisors and upgrade their ore grinding equipment. For smaller operations that can’t afford the 6-12 month lead time and $5 million price tag of a large cryogenic ASU, PSA/VPSA units are transformative because they’re modular: you can add units in chunks as your production grows, instead of having to purchase a whole system upfront.
Then there’s cryogenic ASU tech that’s been re-engineered for efficiency, which is critical for large steel mills. The latest iteration, called “low-pressure cryogenic ASUs,” cuts energy use by 20% compared to 1990s models by optimizing the distillation cycle and recovering heat and nitrogen that was once just vented. I worked with a major steel mill in Pennsylvania in 2021 to upgrade their 40-year-old cryogenic ASU to a low-pressure model. Within six months, their coke consumption per ton of steel fell by another 8%, and their nitrogen waste streams—once a major pollutant—were repurposed for inert gas blanketing in their steel rolling process, eliminating $1.2 million a year in nitrogen purchases from third-party suppliers. That’s the kind of cross-functional impact that most non-metallurgical companies don’t see: an ASU upgrade doesn’t just reduce energy use—it turns a waste product into a revenue stream.
But the most underdiscussed way ASU tech impacts metallurgy is in specialty metal production, where even tiny impurities in gases can ruin an entire batch of metal. Take titanium, a metal used in aerospace and medical implants that’s purified from rutile ore. Titanium production requires 99.999% pure argon for the Kroll process, which turns titanium tetrachloride into solid titanium sponge. If that argon has even 0.1% of oxygen or nitrogen, the titanium becomes brittle and unusable—worthless, because a single batch can cost $200,000 to produce. In 2020, I supplied a custom high-purity argon distillation column integrated with a small cryogenic ASU to a titanium smelter in Alabama that was having 12% of its batches rejected due to gas impurities. After tuning the column’s distillation trays to reduce carryover, their rejection rate dropped to 0.8%—saving them over $1.8 million a year in lost material and rework. For specialty metallurgists, ASU purity isn’t a detail—it’s the difference between profit and operating at a loss.
Of course, no conversation about ASUs and metallurgy today can ignore the elephant in the room: carbon emissions. The metallurgical industry accounts for ~7% of global CO₂ emissions, according to the International Energy Agency, and ASUs alone make up 10-15% of a steel mill’s total emissions because of the energy needed to separate air. The good news is that modern ASU tech is a key part of decarbonizing metallurgy. Let’s go back to that Pennsylvania steel mill I mentioned earlier: after upgrading to a low-pressure cryogenic ASU, their energy use fell by the equivalent of taking 1,200 cars off the road per year. Even more importantly, those repurposed nitrogen streams now power their hydrogen injection system in the blast furnace—hydrogen is a zero-emission alternative to coke, and nitrogen is needed to stabilize the hydrogen combustion, which is a crucial step for the mill to meet its 2030 net-zero goal.
Another area where ASUs are driving decarbonization is in direct reduced iron (DRI) production, a growing method that uses natural gas or hydrogen to turn iron ore pellets into steel without a blast furnace. DRI requires a steady supply of high-purity oxygen to maintain the reduction reaction, and modern ASUs are designed to adjust their oxygen output to match the DRI process’s variable demand. In 2022, I installed a modular cryogenic ASU for a DRI plant in Texas that’s powered by 100% wind energy. The plant’s oxygen is produced using renewable electricity, so the DRI it makes has 60% lower emissions than traditional blast-furnace steel. That steel is now being used for electric vehicle chassis, which means the ASU’s impact ripples all the way from raw ore to the low-carbon cars we drive.
But here’s the thing that most ASU suppliers won’t tell you: even the best technology in the world is useless if it’s not tailored to your specific metallurgical operation. I’ve seen clients buy top-of-the-line cryogenic ASUs that ended up sitting half-idle because their production line only needed 60% of the unit’s capacity. I’ve also seen small operations try to use off-the-shelf PSA ASUs for specialty metal production, leading to costly batch rejections. That’s why my team and I don’t just sell ASUs—we do full site assessments. We’ll walk your mill floor, talk to your blast furnace operators and process engineers, look at your production targets and emissions goals, and build a system that’s calibrated for your needs. Last year, a zinc smelter in Missouri came to me because their old ASU was causing their leaching process to fail 18% of the time. We installed a custom PSA ASU with a built-in humidity control module (a feature most suppliers skip for non-high-purity applications) that cut their leaching failures to 2% and increased their zinc output by 7% in six months. That’s the kind of partnership that makes ASUs impactful, not just a piece of equipment.
Looking ahead, the next wave of ASU tech is going to make this impact even bigger. We’re already testing AI-integrated ASUs that use real-time data from a mill’s furnace, rolling mill, and ore processing line to adjust oxygen, nitrogen, and argon output automatically—no need for manual tuning during shifts. Early tests of these AI systems have shown energy savings of another 15-20% and reduction in gas waste of up to 40%. We’re also working on ASUs that can capture and store excess carbon from metallurgical processes, turning the ASU from a consumer of energy into a contributor to circular economy goals. For metallurgists, this means that in five years, ASUs won’t just support production—they’ll be a core part of your sustainability strategy, not an afterthought.

If you’re a metallurgical plant manager, engineer, or sustainability lead, I know you’re dealing with a lot right now: tight production deadlines, rising energy costs, new carbon regulations, and pressure to meet net-zero goals. The right ASU isn’t just a utility to keep your process running—it’s a tool that can cut your costs, reduce your waste, and future-proof your operation. I’ve been in this industry long enough to know that a lot of suppliers will try to sell you a one-size-fits-all system, but that’s not how you get real impact. If you’re ready to talk about how ASU technology can improve your metallurgical operation, from blast furnaces to specialty metal production, reach out to our team for a no-obligation site assessment and custom proposal.
Compressor And Expander References
International Energy Agency. (2023). The Future of Hydrogen in Industrial Applications. IEA Publications.
American Iron and Steel Institute. (2022). Cryogenic and Modular Air Separation Technologies for Steel Production. AISI Technical Report.
World Steel Association. (2021). Decarbonization Pathways for Global Steel Production. World Steel Association.
Sustainable Aluminium Initiative. (2020). Air Separation Requirements for Low-Carbon Aluminium Smelting. SA Technical Bulletin.
Liu, Y., et al. (2019). Energy Efficiency Advances in Pressure Swing Adsorption Air Separation for Industrial Applications. Journal of Chemical Engineering.
Xinxiang Jiale Intelligent Equipment Co., Ltd.
As one of the most professional air separation unit manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to buy durable air separation unit for sale here from our factory. We also accept customized orders.
Address: No.3913, 9th Floor, Unit 3, East Commercial and Office Complex, Baolong City Plaza, Hongqi District, Xinxiang City, Henan Province, China
E-mail: cc2397410@gmail.com
WebSite: https://www.jiale-asu.com/
