What’s up, food industry folks? Let’s cut to the chase – if you’re relying on a tunnel freezer for your production line, you already know it’s not just about blasting cold air to freeze stuff fast. The real make-or-break for your product quality, yield, and even energy bills? Freezing uniformity. Spots where veggies are ice crystals way too big, or a batch of chicken nuggets has a few pieces still warm in the center? That’s not just annoying – that’s wasted product, missed shelf life, and frustrated customers. Tunnel Freezer
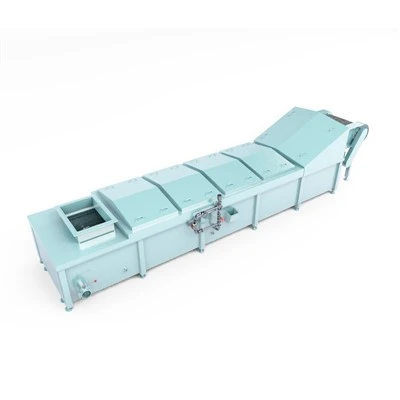
I’m part of a team that’s built tunnel freezers for years, and I’ve talked to plant managers who’ve thrown out full pallets because of inconsistent freezing. Today, let’s break down how that uniformity actually works, no boring engineering jargon, and throw in some real-world stuff we see every day.
First, let’s get on the same page: what even is “uniform freezing” in a tunnel freezer? It’s not every single piece freezing at the exact same millisecond. That’s impossible, even with the best tech. It’s every item (or every part of every item) hitting the target core temperature at the same time, no cold spots that leave half a batch under-frozen or hot spots that burn the edges. For example, if you’re freezing a 2oz chicken patty, the core needs to get to 0°F quickly, but if the outside freezes way too fast, you get that crumbly texture or ice crystals that ruin the bite. On the flip side, if the middle stays warm, bacteria could be hanging out long enough to be a food safety risk. Not cool.
So how do we pull that off? Let’s start with the air flow – it’s the backbone of the whole system. A lot of people think “more cold air = faster freeze” but that’s wrong. It’s about how that air moves, not just how much there is. Think of your house AC: if one vent is blowing directly at your couch and another in the corner is weak, some rooms are freezing and others are stuffy. Tunnel freezers have that same problem if the air isn’t engineered right.
We design our units with high-velocity fans, not just big ones – these blow tiny, fast-moving cold air streams that don’t just hang out in one spot. But here’s the secret sauce: we don’t put the fans just at the start or end of the tunnel. We space them evenly along the length, and angle them so they sweep across the product conveyor, not straight at it. Why? If air blasts straight at frozen food, it can form a thin layer of ice on the surface that insulates the inside. That’s called “freezer burn initiation” – not good. Angled, swirling air breaks that surface layer up as it forms, so cold air can keep hitting the product evenly.
Also, we adjust air direction based on what you’re freezing. If you’re freezing small, flat stuff like french fries, we angle the fans to blow horizontally across the conveyor. For thicker items like meat patties or whole fish, we tilt some fans downward to get under the product, since cold air sinks. Skip that, and the bottom of a pallet of burgers will freeze slower than the top – we see that all the time in budget freezers that don’t get air flow right.
Next, product handling. You can have the best air flow in the world, but if your product is piled unevenly or jumbled on the conveyor, uniformity goes out the window. Let’s say you have mixed sizes of broccoli florets – some are 1 inch, some are 2 inches. The smaller ones will freeze way faster, and if they’re stacked on top of bigger ones, the big ones get less air. We work with clients all the time to tweak conveyor settings: mesh belts instead of solid ones, so air flows through, not around, and we’ll even add infeed dividers to spread product evenly, no clumps. If you’re freezing bulk pallets, we can set up layer spacers so air gets between every layer, not just the top. That’s a game-changer – I’ve seen a client go from 15% reject rate to 2% just by fixing their product distribution, no new freezer needed.
Temperature control is another big one, and not just the freezer’s air temp. We use what’s called a cascade refrigeration system, but let’s keep it simple: instead of one big cooling loop, we have two. The first loop cools the air down super low (like -40°F or even lower), and the second loop keeps that air consistent. A lot of cheap tunnel freezers use a single loop, which can spike in temp when the load is heavy. For example, if you’re shoveling 1000 lbs of chicken into the tunnel at once, the single loop might drop temp to -20°F for a few minutes, leaving half the batch under-frozen. Our system keeps temp within ±1°F along the entire tunnel, no dips, no spikes. We also add multiple temp sensors – not just one at the entrance, but every 10 feet along the conveyor, so if a spot is off, the fan speed adjusts automatically. That’s a lot better than old manual systems where someone has to walk around checking temp every hour.
Wait, let’s talk about product-specific tweaks because that’s where a lot of suppliers cut corners. A tunnel freezer isn’t one-size-fits-all. If you’re freezing delicate berries, you don’t want high-velocity air because it’ll bruise them. So we’ll dial back the fan speed and adjust the angle to be gentler, while still keeping air uniform. For dough products like pizza bases, you need air that’s not too dry, right? If it’s too dry, the crust cracks. So we add a humidity control module that keeps moisture levels consistent, so the outside freezes at the same rate as the inside, no cracks. For raw meat, we need to keep the surface clean of pathogens, so we adjust air flow to prevent cross-contamination from earlier batches. A lot of generic tunnel freezers can’t do that, so clients have to compromise on product quality to get uniformity – that’s not how we roll.
Let’s add a real example to make this concrete. Last year, we worked with a frozen vegetable producer that was getting complaints from grocery stores about “frosty ends” on their green beans and inconsistent core temps. They were using a budget tunnel freezer with solid conveyor belts and fans only at the exit. The result: the top layer of beans froze fast, the bottom layer was still warm, and clumps of beans in the middle didn’t get enough air. We swapped out the solid belt for a mesh one, added 4 mid-tunnel fans angled to blow upward from below the conveyor, and calibrated the temp sensors. Within a month, their reject rate for beans dropped 12%, their freeze time was cut by 20%, and their energy use went down 15% because we weren’t wasting extra cold air on cold spots. The plant manager told us that saved them over $40k a year – that’s the kind of win we care about.
Now, what are the common mistakes we see that kill uniformity? First, under-sizing the freezer for production. If you’re running more product than the tunnel was designed for, you’re cramming more into the same space, so air can’t circulate. Second, ignoring conveyor speed. If the conveyor is too fast, some product doesn’t stay in the cold long enough; too slow, and some sits longer. We use variable speed drives that sync with your production line, so every item spends exactly the right amount of time in the tunnel, no matter how fast your line is running. Third, not doing regular maintenance. Fans get dirty, sensors get clogged with ice, air filters get backed up. We tell all our clients to do a quick check weekly: wipe down sensors, make sure fans aren’t making weird noises, check that the mesh belt isn’t torn. That small stuff keeps uniformity consistent for years.
Wait, also, what about the “critical freeze point”? That’s the range where most water in food turns to ice – usually between 32°F and 25°F. If you can get through that range fast and evenly, you get smaller ice crystals, which means better texture. If you go through it slow, ice crystals get big and break cell walls, so when you thaw the product, it’s mushy. Uniform freezing means every item hits that critical point at almost the same time, so the texture is consistent across the whole batch. That’s why a lot of artisanal frozen food brands insist on tunnel freezers – they don’t want their frozen spinach to taste like slimy mush when heated.
Let’s be real, no system is perfect. Even the best tunnel freezers will have tiny variations, but the goal is to keep them within industry safety standards and quality expectations. We’ve had clients come to us saying their old freezer had a 10°F temp difference from one end to the other – that’s a disaster. Our units keep that difference under 2°F, every single time.
If you’re dealing with inconsistent freezing – whether it’s high rejects, bad texture, food safety scares, or wasted energy – you don’t have to settle for it. We’ve helped dozens of producers fix their uniformity issues, from small craft operations to big national brands. Whether you’re freezing produce, meat, seafood, baked goods, or anything in between, we can design a tunnel freezer that fits your line, your product, and your budget, without cutting corners on the stuff that actually matters.

If you’re ready to stop throwing out half-batches and start getting uniform, high-quality frozen product every time, reach out to us to chat through your needs. No sales pitches, no hidden fees, just real advice for your specific operation.
Food Processing Line References
Fellows, P. (2017). Food Processing Technology: Principles and Practice. Woodhead Publishing.
Sperling, J. (2020). Industrial Freezing of Foods: Fundamentals and Applications. CRC Press.
Trog, T. (2019). “Uniformity in Tunnel Freezing: Key Factors for Product Quality.” Journal of Food Process Engineering, 42(5), e13127.
Shaoxing Kanglong Rerrigeration and Fanner Equipment Co., Ltd.
As one of the most professional tunnel freezer manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to wholesale advanced tunnel freezer made in China here from our factory. Also, custom service is available.
Address: No.1,Lide Road,Shangpu Industry
E-mail: sales@iqffreezercn.com
WebSite: https://www.iqffreezercn.com/
