If you’re running a UV coating line, you know coating speed makes or breaks your output. Mess it up, and you’ve got uneven coats, cured spots that are still tacky, or worse—wasting raw materials that cut into your margins. I’ve been selling UV coating lines for over 12 years, and let me tell you, most clients hit a wall with speed adjustments because they’re either guessing or following generic guides that don’t account for their specific line or products. Today, I’m breaking down exactly how to nail that adjustment, no fluff, just the stuff that actually works. UV Coating Line
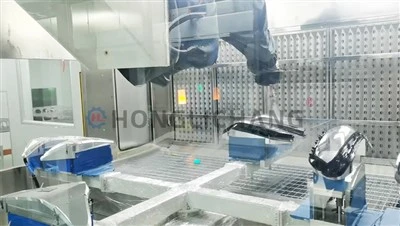
First, let’s cut to why speed even matters here. UV coating works by two key steps: first, the wet coat gets applied to your substrate (could be wood, metal, plastic, even paper), then it zaps with UV bulbs to cure instantly. Speed dictates two big things: how much liquid coats stays on the substrate (that’s your coat thickness) and how much UV light hits that liquid before it moves on. Mess that balance, and you’re either under-coating (chipping, poor adhesion) or over-coating (running through too much coating, excess waste).
I’ve had clients show up thinking “faster = more output” which is true, but only up to a point. Push speed too hard, and the UV exposure time drops. UV bulbs don’t just work on intensity—they need time to trigger the photoinitiators in the coating, right? If the line is zooming, each spot only sits under the bulbs for a fraction of a second. Those photoinitiators never fully activate, so the coat stays sticky, or cures on the surface but not all the way through—leading to peeling later, especially if the product’s going through heat or moisture down the line.
So where do you start? Skip the random numbers, grab your actual setup. First, pull two specs off your line: the length of your UV curing chamber, and the intensity of your bulbs. Most modern UV lines have bulb intensity printed on the label, but if it’s old-school, grab a cheap UV intensity meter—they’re not expensive, and way more accurate than guessing. Let’s do a quick math check here to get your baseline: your UV exposure time is just chamber length divided by line speed. For example, if your chamber is 10 feet long, and you run at 50 feet per minute, your exposure time is 0.2 minutes, or 12 seconds. If you crank speed to 75 feet per minute, that drops to 8 seconds. That’s a huge swing in curing time, and it’s the main reason speed can’t be set blindly.
Next, factor in your coating type. Not all UV coatings are the same. I’ve seen clients use a glossy acrylic coating for wood, then turn around and run the same speed for a matte epoxy on metal, and wonder why it’s not curing. Epoxy coatings usually have slower-reacting photoinitiators, so they need longer exposure time—meaning you can’t run as fast as you would with a fast-curing acrylic. Same goes for substrates: porous ones like cardboard will absorb more coating, so you might need a slightly faster speed to keep coat thickness consistent, while non-porous like aluminum will hold more, so slower speed to avoid drips.
Now, let’s walk through the step-by-step process I walk all my clients through when they’re adjusting speed. No jargon, just actionable steps:
Step 1: Do a test run with a scrap sample. Grab a piece of your actual substrate (don’t use a random piece of cardboard, use the exact material you’re coating) and run it through your line at the middle speed you think you’ll use—say, if you usually run between 40 and 60 feet per minute, start at 50. Don’t forget to run the test with the exact coating you’re using, too. Apply the coat, let it cure, then check two things: tackiness and thickness. For tackiness, run your finger gently across the cured surface—if it leaves a smudge or feels sticky, you’re going too fast, not getting enough UV exposure. If it’s hard as a rock, good. For thickness, use a micrometer to measure before and after coating, or do the simple “wipe with solvent” test: take a small cotton swab with isopropyl alcohol, rub a tiny spot on the cured coat. If it comes off easily, you’re either too fast (un-cured material rubbing off) or too slow (excess coating building up). If it doesn’t come off, your thickness is right.
Step 2: Tweak speed in small increments. I see clients do this wrong all the time—they jump from 50 to 70 in one go, then wonder why everything’s messed up. Instead, adjust by 5 feet per minute at a time. Once you get a good test at 50, try 55: run another scrap, check tackiness and thickness. If it’s still perfect, bump to 60. If it’s sticky, drop back to 55, maybe your sweet spot is there. For most standard applications, the sweet spot is where your coat thickness is within 0.1 to 0.5 mils (that’s the industry standard for most coatings) and you get full cure without extra material waste.
Step 3: Adjust for volume, not just speed. Wait, that sounds counterintuitive, right? But here’s the thing: if you need more output, don’t just crank speed—you might need to adjust the coating applicator gap too. If you run faster, the applicator (whether it’s a roll coater, curtain coater, or spray gun) will lay down less coating automatically, so if you don’t widen the gap a little to compensate, your coat will be too thin. I had a client last month who ran his line at 20% faster than usual, skipped widening the roll coater gap, and ended up with 30% of his first batch chipping because the coat was too thin. That’s a $5k mistake, all because he ignored that little step.
Now, what about common issues that pop up when adjusting speed? Let’s cover the big ones I get asked about every week:
First, tacky coating after curing. 9 times out of 10, this is too fast. Your UV bulbs aren’t reaching the full thickness of the coat, so the surface cures but the inside stays sticky. The fix here is to drop speed by 5 to 10 feet per minute, or bump up your bulb intensity if you can (if you’re using old bulbs, they lose intensity over time—replace them every 12 months, or you’ll be chasing speed adjustments forever).
Second, uneven coating. If your coat is thicker on one end than the other when you speed up, that’s usually a combination of too fast and a misaligned applicator. When speed increases, the curtain coater or roll will distribute coating differently, so double-check that your applicator is aligned evenly across the width of your substrate. Sometimes speeding up just amplifies a small applicator issue you didn’t notice at slower speeds.
Third, material waste. If you’re going too slow, you’re laying down more coating than you need. A friend of mine runs a custom cabinet shop, and he told me he used to run his UV line at a crawl because he was scared of under-curing. Once we adjusted his speed to his exact sweet spot, he cut coating waste by 18%—that’s $12k a year he’s not throwing away. It’s a no-brainer, but people get stuck in the habit of running slow “just in case.”
Another thing I can’t stress enough: log every adjustment. When a client calls me six months later saying “my line’s acting weird,” I ask for their speed logs, and 90% of the time, they can’t remember what speed they were running, or what coating they used. Keep a simple notebook (or a spreadsheet, whatever works) that notes: speed, coating type, bulb intensity, substrate, and the results (cure quality, thickness, waste). That way, when you switch to a new coating or new substrate, you don’t have to start from scratch. I have a client who’s been logging for 3 years, and he can adjust to a new product in 10 minutes instead of an hour, no test runs needed.
Wait, what about web coating vs. sheet coating? A lot of people mix these up. If you’re running a sheet UV line (like for wood panels), your speed adjustment is a little different because the sheets are separate—you have to make sure there’s enough space between sheets so they don’t rub together as they move through the curing chamber. If you’re running a web line (continuous, like for plastic film), you have to account for tension on the web—too fast, and the web stretches, leading to uneven coats. I always tell web line clients to adjust tension when they adjust speed, not just the other way around.
Let me give you a real example. Last quarter, a client who manufactures outdoor metal signs reached out. He was running his line at 65 feet per minute, and his signs were peeling after 6 months, especially in rain. We went through his process: he was using a high-gloss UV urethane coating, substrate was galvanized steel, bulb intensity was 80 W/cm. We calculated his exposure time: chamber was 8 feet, so 65 fpm = ~7.4 seconds. We dropped his speed to 55 fpm, adjusted the roll coater gap from 0.008 inches to 0.010 inches, and his exposure time went to ~9.5 seconds. Result? His peel rate dropped from 12% to 0.2%, and his coating waste went down 10%. He was blown away, said he’d been running too fast to hit a high output number he was told was “industry standard,” but that number didn’t account for his specific product.
So what’s the takeaway here? Adjusting UV coating speed isn’t about hitting a random number someone told you, it’s about matching three things: your line’s specs, your coating type, and your substrate. Skip the guesswork, do test runs on scrap, adjust in small increments, and don’t forget to tweak your applicator gap too. And for the love of all things coating, replace your bulbs regularly—old dim bulbs will mess with every speed adjustment you make.
If you’re still stuck, whether you’re troubleshooting a stubborn line or setting up a new UV coating line and need help dialing in the right speed, hit me up. I’ve helped hundreds of clients across industries nail their speed adjustments, so I can walk you through your specific setup no matter what you’re coating. Don’t waste money on bad batches or excess material—let’s get your line running perfectly.
Turnkey Paint Line References:
- UV Coating Technology: Principles and Applications, Surface Coatings International, 2021
- Industrial UV Curing: Equipment, Processes, and Troubleshooting, SME, 2020
- Coating Speed Adjustment for Roll Coating Lines, Coating Technology Association, 2019
Shenzhen Honglichang Machinery Manufacturing Co., Ltd.
We are one of the most professional uv coating line manufacturers and suppliers in China, also support customized service. Please feel free to buy advanced uv coating line for sale here from our factory. Welcome to contact us for quotation.
Address: No. A802, Building 2, Tianan Digital Plaza, Longgang, Shenzhen, China
E-mail: victor@honglichang.com
WebSite: https://www.honglichang-paint.com/
